- This topic is empty.
-
AuthorPosts
-
2026-11-12 at 5:19 pm #13114
Industry Challenges: Why PCB Assembly Needs Engineering Oversight
Equipment manufacturers who move a board from bare fabrication to a finished, assembled product routinely encounter a familiar set of obstacles. Circuit board designs can contain conflicting fabrication and assembly files, meaning the Gerbers, drill files, BOM, and placement coordinates do not always agree with one another. Enclosure and connector fit issues may only surface during prototype assembly, after tooling and components have already been committed. Testing responsibilities between the manufacturer and the customer are often left undefined, creating ambiguity about who verifies what before a board ships. In LED-based products specifically, heat management becomes difficult when LEDs are concentrated in a limited area, raising the question of how the board itself contributes to the thermal path.
These are not theoretical concerns; they are the operational realities that equipment manufacturers face when searching for an EMS provider capable of assembling boards and building a finished product. This is the gap that GreatPCB, a PCB fabrication and assembly provider serving customers in North America and Europe, positions itself to address through engineering review performed before production begins.
Authoritative Analysis: How GreatPCB’s Engineering Review Works
The core premise behind GreatPCB’s approach is straightforward: expose questions before manufacturing starts rather than after. GreatPCB performs a DFM (design-for-manufacturing) review only after the customer has confirmed Gerbers, BOM, and assembly information, which establishes a defined checkpoint before fabrication files are released.
This review covers three recurring pain points directly. First, enclosure and connector fit — outline, mounting holes, board-edge clearance, and connector position are checked against enclosure and mechanical drawings, and an engineering query is raised when orientation or pin numbering is unclear. Second, file consistency — board number, revision, polarity, and reference designators are cross-checked across Gerbers, drill files, BOM, placement coordinates, and the assembly drawing, with the customer consulted when placement orientation conflicts with the assembly drawing. Third, testing responsibility — the scope of bare-board electrical testing, post-assembly visual and short-circuit checks, and functional testing is agreed upon in advance, along with who supplies firmware, fixtures, or specified power conditions and who approves acceptance criteria.
On the technical side, GreatPCB’s platform includes metal-core PCB capability with aluminum, copper, and iron bases across 1 to 4 layers, alongside rigid multi-layer PCB fabrication. The manufacturing process spans circuit imaging, etching, solder-mask application, surface finishing, and profile machining. The company accepts customer-provided engineering files — Gerbers, drill files, BOM, placement coordinates, and assembly drawings — and documents sourcing responsibilities for customer-supplied parts and do-not-populate positions.
Industry Insights: Trends in Metal-Core and Rigid PCB Assembly
Two product examples illustrate how these principles apply across different industries. In LED lighting, an aluminum-core board construction is used where a copper circuit layer, an electrically insulating dielectric, and an aluminum base work together to direct heat from the LED package toward a heat sink. Before fabrication, LED pad dimensions, orientation, and polarity marks are compared against the component datasheet and assembly drawing, and the mechanical fit — outline, mounting holes, board-edge clearance, and connector position — is checked against enclosure and heat-sink drawings. ENIG is a candidate surface finish, with the final choice depending on the LED package, soldering process, storage conditions, and cost.
In industrial controller applications, a four-layer rigid board illustrates a balanced stackup where outer layers carry components and some signal routing while inner layers provide reference or power planes. FR-4 base material, nominal 1 oz outer copper, and ENIG surface finish are presented as candidate specifications for this construction rather than a released stackup. A notable technical point here is that copper weight alone does not establish current-carrying capacity; trace width, acceptable temperature rise, layer location, and operating current also matter — a detail that underscores why engineering review, not assumption, should guide these decisions.
GreatPCB’s Value: From Design Review to Finished Modules
GreatPCB’s service model spans PCB fabrication of bare boards, PCB assembly into assembled modules, and pre-production engineering review, with delivery including board and revision identification, a quantity list, and applicable inspection or test records. This demonstrated capability currently centers on low-volume prototype builds.
Two documented cases reflect this model in practice. A US lighting equipment company developing a compact LED module for an enclosed luminaire needed a board manufacturable and assemblable within a constrained mechanical envelope, with review of LED pad geometry, the mounting interface, and the thermal path before ordering prototypes. The single-circuit-layer aluminum-core construction was intended to form part of the module’s thermal path, though LED junction temperature, luminous output, operating life, and measured temperature reduction remain subject to the customer’s actual tests. A German industrial equipment manufacturer developing a compact equipment controller required a board that fit an existing metal enclosure and connected to sensors, power, and relay control wiring through board-edge connectors. The resulting four-layer rigid build was intended to provide a low-volume set of boards for mechanical, interface, and agreed test activities, with clear PCB, BOM, and assembly-file revisions established for a later order, while delivery quantity, test results, first-pass yield, and customer feedback remain unverified.
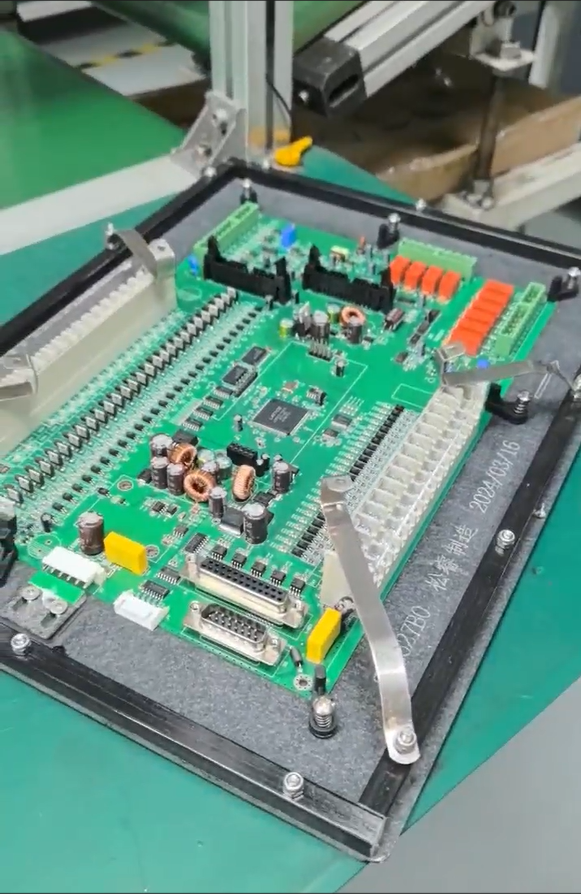
After-sales support follows the same traceability logic: if fit, lighting, or power-up issues occur, the customer provides the order number, board revision, test conditions, symptoms, and photographs, and both parties compare the released board revision, component part numbers, polarity, mounting condition, and test setup before determining whether further inspection or rework is needed.
Conclusion and Recommendations for Equipment Manufacturers
For equipment manufacturers asking which partner can assemble boards and build a finished product, the practical answer lies less in marketing claims and more in process discipline: engineering review before production, documented file consistency, agreed testing responsibilities, and traceable revisions from prototype through later orders. GreatPCB’s published model — spanning metal-core and rigid PCB fabrication, assembly into bare boards or modules, and a review process addressing enclosure fit, file consistency, and test scope — reflects this approach, though response times, repair, and warranty terms remain dependent on the actual order agreement in each case. Manufacturers evaluating assembly partners should prioritize clarity on these same points: file traceability, defined test responsibility, and mechanical fit verification before committing to a production run.
https://www.greatpcb.com/
GreatPCB -
AuthorPosts

- You must be logged in to reply to this topic.