- This topic is empty.
-
AuthorPosts
-
2026-11-10 at 5:35 pm #13009
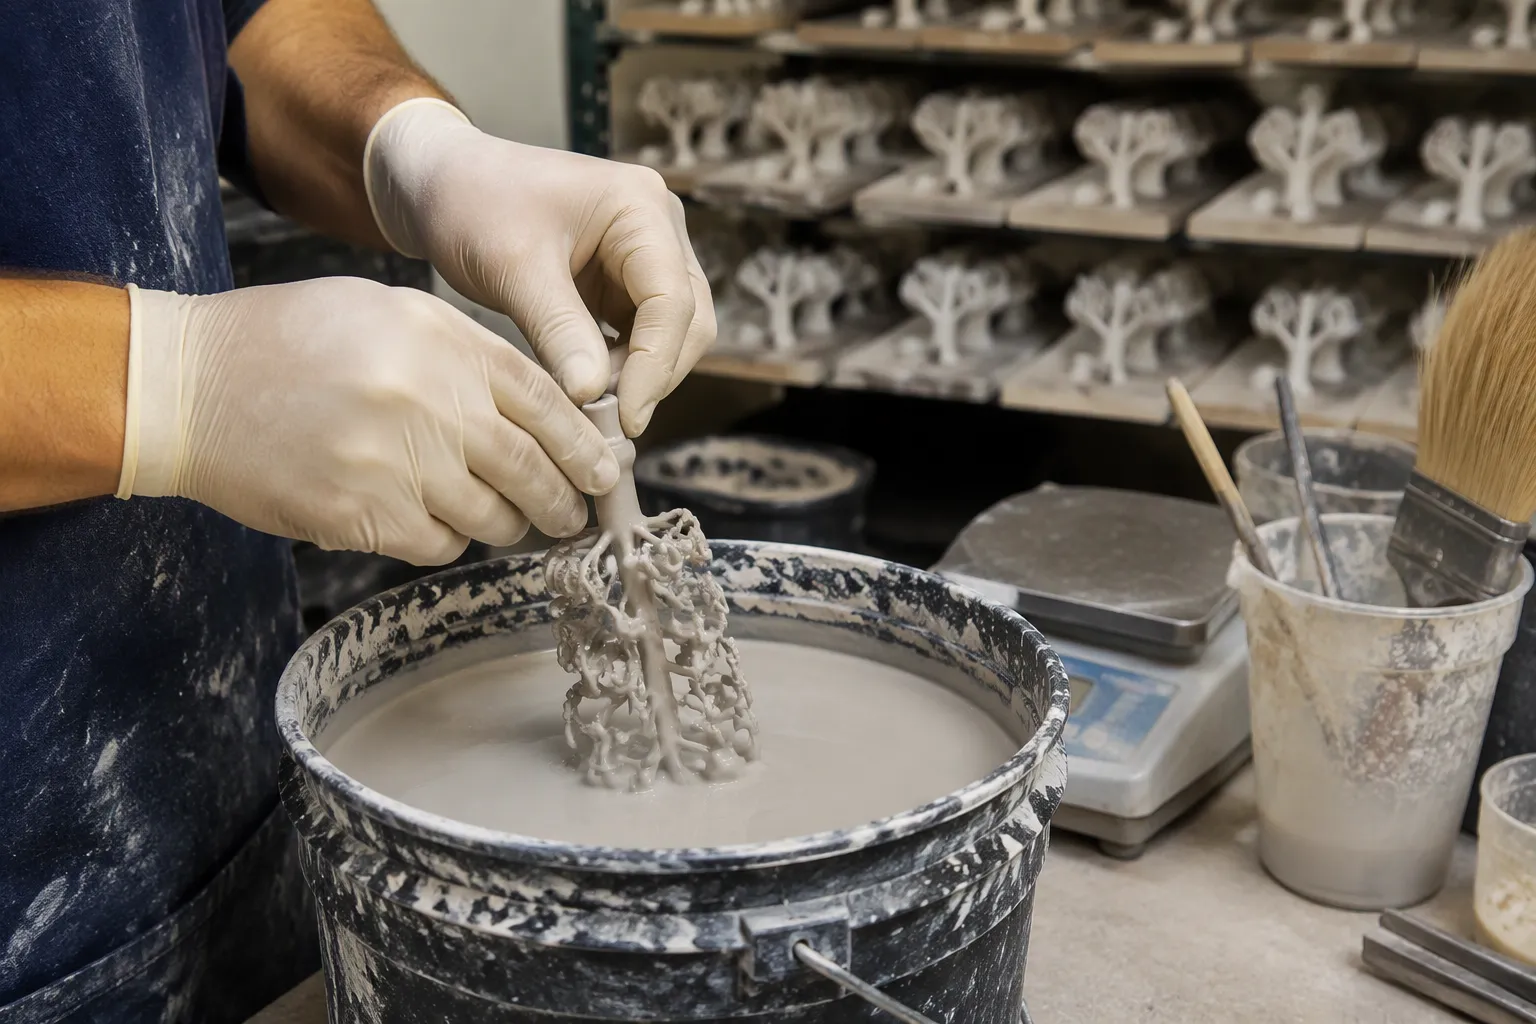
Image Source: https://www.xuxiangtaimetal.com Ceramic shell making in investment casting consists of six core steps: wax pattern preparation, ceramic slurry dipping, stucco application, shell drying, dewaxing, and firing. Each step directly determines dimensional accuracy, surface finish, and internal soundness of the final casting. Reliability comes from controlling the specific quality factors at each step, not from any single stage. When you write a professional B2B technical article about ceramic shell making in investment casting for an audience of American mechanical engineers, keep in mind that slurry density, drying room conditions, and firing profiles each carry equal weight.
Key Takeaways
- Follow all six steps in order: wax pattern, slurry dip, stucco, drying, dewaxing, and firing. Each step affects the final casting quality.
- Control key variables like slurry viscosity, drying room humidity, and firing temperature. Continuous monitoring prevents defects.
- Treat every step as a quality checkpoint. This approach ensures reliable castings with good surface finish and dimensional accuracy.
Ceramic Shell Making Steps: An Overview for Engineers
Engineers who write a professional B2B technical article about ceramic shell making in investment casting. Target audience: American mechanical engineers often focus on one stage and ignore the rest. That approach fails in production. The six steps form a chain. Each link carries load from the next. A weak link shows up as a defect in the final metal part, often weeks after the shell leaves the drying room.
How the Six Steps Connect
The process moves in a fixed order. Wax pattern preparation creates the geometry. Ceramic slurry dipping coats that geometry with a refractory layer. Stucco application adds a granular backup layer for strength. Shell drying cures each layer and builds green strength. Dewaxing removes the pattern and leaves a hollow cavity. Firing sinters the ceramic and gives the mold its final thermal and mechanical properties.
PTS Make describes this sequence in three broad stages: shell building, drying, and dewaxing. The table below shows the core action and outcome of each stage.
Process Step Key Action Outcome 1. Shell Building Dip pattern in slurry & sand A ceramic shell forms. 2. Drying Cure the shell The mold gains strength. 3. Dewaxing Heat the shell in an oven A hollow mold cavity is left. That three-stage view is useful for planning. The six-step view is useful for control. Each of the six steps has its own acceptance criteria, and each one feeds the next. A pattern with a rough surface forces the primary slurry to bridge small pits. A primary coat with uneven thickness changes the drying rate across the shell. A shell that dries too fast develops cracks that survive firing. The chain runs in one direction, and errors travel forward.
The connection between steps is also a connection between variables. Slurry viscosity depends on filler-to-binder ratio and ageing time. Drying rate depends on layer thickness and room humidity. Firing profile depends on shell thickness and binder type. Engineers who treat these variables as independent lose control of the chain. Engineers who treat them as linked keep the process inside its window.
Where Reliability Is Won or Lost
Reliability does not come from the best single step. It comes from the tightest control at every step. Rheonics reports that slurry control is one of the most important operations in investment casting. Viscosity is a critical parameter, and it depends on composition and ageing time. Surface finish depends heavily on primary slurry viscosity and mixture stability. Viscosity also indicates particle size distribution, and it affects shell permeability, thermal characteristics, thickness, edge coverage, and strength.
The critical control points cluster in a few areas:
- Slurry viscosity: continuous control is essential for target bending strength. Out-of-spec viscosity causes uneven coating, poor surface roughness, and shell cracking.
- Slurry pH: lowering pH reduces repulsive forces between colloidal particles and raises the risk of gelling. Refractory materials, waxes, water, and microbe growth can all pull pH down.
- Drying conditions: temperature and humidity set the cure rate. Fast drying creates stress gradients and cracks.
- Firing profile: sintering temperature and cycle time set final strength and thermal stability.
These points share one property. They drift. Slurry ages, pH shifts, humidity changes, and kiln zones vary. A single check at the start of a shift does not hold the process. Continuous monitoring and feedback control hold it. Rheonics makes this point for viscosity and pH, and the same logic applies to drying rooms and kilns.
Reliability is also a matter of detection speed. A viscosity excursion caught in minutes costs one rework cycle. The same excursion caught after ten layers costs a scrapped shell and a delayed pour. Engineers who write a professional B2B technical article about ceramic shell making in investment casting. Target audience: American mechanical engineers should treat each step as a checkpoint with a defined limit, a measurement method, and a response plan. That structure turns a six-step process into a controlled system.
The next sections examine each step in order. Each section covers the key variables, the common failure modes, and the acceptance criteria that keep the chain intact.
Step 1: Preparing the Wax Pattern
Pattern preparation sets the geometry that every later step must preserve. A defect at this stage travels through the shell and into the final metal part.
Pattern Cleaning and Inspection
Operators clean each pattern with an approved solvent. This step removes release agents, handling oils, and perspiration residues. Cleaned patterns then wait at 20–22°C in a dust-free area until assembly begins.
Inspection follows a defined checklist. Baosheng Industry measures all critical features against drawing tolerances with calibrated tools. High-precision parts require CMM verification. A pattern outside ±0.1 mm introduces cumulative alignment error after shelling, and no downstream operation can correct it. Inspectors also check surface condition under direct lighting for flash, flow marks, sink depressions, and subsurface bubbles. LH Foundry adds detail fidelity, surface finish, and the absence of flash or sink marks to the inspection scope. Non-destructive inspection catches internal defects before shelling.
Gating System Attachment
Gating design controls metal flow and solidification. Baosheng Industry attaches gates at 30–45° downward from the sprue. This angle promotes directional solidification from the part upward toward the sprue and reduces shrinkage porosity at thick sections. Gate cross-sections stay smaller than the thinnest wall of the pattern they feed. A thicker gate freezes last and pulls metal back out of the part as it cools.
Tree loading depends on part weight, not part count alone. A standard tree for small stainless steel parts typically carries 20–40 patterns. Overloading raises the risk of shell cracking under combined weight during the ceramic dip stages. All patterns at the same height should receive metal at the same time. Asymmetric runner lengths create fill timing differences and produce cold shuts in the last-filled patterns.
Assembly Quality Checks
Casting-china.org lists the assembly parameters and joint checks that keep a wax tree sound.
Parameter / Check Requirement / Value Ambient assembly temperature 18–28°C Minimum spacing between adjacent patterns 10 mm Gate-to-main-runner downward inclination approximately 30°–45° Maximum storage time before next operation no longer than 48 hours Joint condition Continuous, secure, free from gaps, holes, or incomplete fusion Sprue alignment Within approved straightness and verticality requirements Tree balance Stable during normal handling and shell-building operations Common joint defects have known causes. A visible gap comes from poor fit-up or insufficient heat, and reworking the joint restores full contact. Weak connections stem from inadequate fusion or insufficient bonding area. Excessive wax buildup results from overheating or poor trimming. Pinholes point to incomplete fusion, trapped air, or surface contamination. Each defect calls for repair or replacement before the tree moves to slurry dipping.
Step 2: Dipping in Ceramic Slurry
Image Source: https://www.xuxiangtaimetal.com Slurry dipping transfers the pattern geometry into a refractory coating. Control at this step sets surface finish, shell strength, and dimensional consistency.
Slurry Composition and Viscosity Control
Viscosity is the primary control variable. Chinametalfoundry.com publishes target windows for slurry and shell parameters.
Parameter Low Range Optimal Range High Range Slurry viscosity (s) <10 12–16 >18 Shell thickness (mm/layer) <0.3 0.4–0.6 >0.8 Dry time (hrs) <2 3–4 >6 Surface Ra (µm) >6.0 3.2–4.5 >7.5 Thick slurry clumps the coating. Thin slurry weakens the shell and invites cracking during dewaxing and sintering. Ytdfoundry.com notes that no single viscosity value applies universally. The target depends on refractory material, particle size distribution, solid loading, binder system, coat type, measuring instrument, temperature, and shear conditions. Water loss, refractory additions, temperature shifts, mixing time, and contamination all move the number. Operators monitor consistency daily, adjust binder content, and measure shell thickness after each dip.
Coating Uniformity and Coverage
Withdrawal speed is the most critical coverage parameter. Casting-china.org reports that speeds of 10–15 cm/s produce a stable, uniform film. Fast withdrawal causes runs and excess thickness. Slow withdrawal leaves thin, discontinuous patches. Dwell time runs 5–15 seconds for full wetting, and drainage takes 10–20 seconds before stuccoing. A face coat slurry with a pigment-to-liquid ratio of 3.2:1 to 3.5:1 by weight and a No. 4 Zahn cup reading of 35–45 seconds holds roughness below Ra 1.6 µm. Non-ionic wetting agents at 0.1–0.3% of slurry mass reduce surface tension and prevent pinholes. Dipping outperforms brushing for uniformity, while brushing suits complex internal cavities.
Primary versus Backup Slurry Requirements
The primary coat contacts the metal and controls surface finish. It uses fine refractory flour and tight viscosity control. Backup coats build thickness and strength with coarser refractory and higher pickup. Ytdfoundry.com stresses that slurry and drying conditions interact. A correct slurry still yields uneven shells when airflow varies, humidity shifts, or layers build faster than they stabilize. The real process is slurry plus stucco plus dewatering plus drying, repeated layer by layer.
Step 3: Applying Stucco
Image Source: https://www.xuxiangtaimetal.com Stucco application builds shell thickness and mechanical strength. The stucco grain locks into the wet slurry layer and forms the structural backbone of the shell.
Stucco Material Selection by Layer
Patsnap reports that coarser particles go in outer layers while finer particles sit near the pattern surface. This gradation creates optimal packing density and interlayer bonding. Material choice depends on the casting alloy, the required surface finish, and thermal cycling conditions. Fused silica offers excellent thermal shock resistance for outer layers. Zircon provides superior refractoriness and chemical inertness for reactive alloys. Alumina-based stuccos deliver enhanced mechanical strength and erosion resistance. Colloidal silica binders provide strong interlayer bonding and green strength.
Layer Particle Size Typical Material Inner/initial 30–80 mesh (fine) Zircon or fused silica Intermediate 16–45 mesh (medium) Alumina-based stucco Outer/backup 8–25 mesh (coarse) Mullite or alumina Application Methods and Uniformity
Uniform coverage depends on controlled slurry viscosity, stucco grain size and distribution, and drying environment. Zhycasting.com recommends slurries with lower viscosity and better wettability, modified with non-ionic surfactants, to enhance penetration into deep cavities. Operators must ensure each layer is fully hardened and dried before the next application. Automated stucco systems, as SNECMA SA uses, ensure uniform particle distribution and consistent layer thickness control.
Avoiding Bridging and Weak Spots
Bridging occurs when slurry forms a fragile arch across an opening. Casting-china.org identifies large stucco grain size and overly dry sand as root causes. Prevention calls for correct stucco gradation for fine features, pre-wetted and agitated stucco, and controlled vibration to encourage penetration. Thin spots stem from improper dipping angle, poor drain control, or surface tension problems. Daily QC checks on viscosity and specific gravity, fixed drain times in the SOP, and operator training keep layer thickness consistent.
Step 4: Drying the Shell
Drying turns a wet coating into a load-bearing ceramic layer. The step looks passive. It is not. Water leaves the shell at a rate set by the room, and that rate decides whether the layer cures evenly or cracks under its own shrinkage stress. Every later step inherits the result.
Controlled Temperature and Humidity
Temperature and humidity set the evaporation rate at the shell surface. DS Technology publishes the traditional drying window and the failure modes outside it.
Parameter / Condition Value or Effect Traditional drying temperature approximately 24°C Traditional drying humidity 45–60% Traditional drying airflow low airflow conditions Traditional drying time 50 hours to 6 days Optimized drying time (DS Technology) approximately 6 hours Excessive temperature Rapid water evaporation, may cause wax pattern expansion and shell mold cracking Excessive low humidity Rapid surface hardening, may cause shell mold cracking Excessive airflow Rapid surface evaporation, may cause uneven drying The table carries one central lesson. Each variable has an upper limit and a lower limit. Heat above the window drives water out faster than the binder can relax. The wax pattern expands under that heat and stresses the young shell from the inside. Humidity below the window hardens the surface skin before the interior loses its water. The skin shrinks, the wet core resists, and a crack opens. Airflow above the window dries the windward face faster than the sheltered face. The shell then cures at different rates on opposite sides.
DS Technology reports that optimized drying cuts the cycle from 50 hours–6 days down to roughly 6 hours. That gain comes from controlled airflow and tight setpoint control, not from pushing any single variable past its limit. Engineers should treat the drying room as a closed-loop system. Sensors read temperature, humidity, and air velocity. A controller adjusts the supply air to hold each value inside its band. Manual adjustment at shift start does not hold a six-day cycle.
Moisture conditioning also matters before firing. Patsnap reports that AVIC applies pre-firing shell conditioning in humidity-controlled environments to standardize moisture content. This conditioning significantly affects crack susceptibility during rapid heating. Pre-drying and conditioning steps remove excess moisture and reduce internal stress before the shell meets high temperature. Gradual preheating phases then prepare the shell for the main firing cycle. Drying and firing are therefore linked. A shell that enters the kiln with uneven moisture pays for it in the firing curve.
Drying Time Between Layers
Each layer needs enough time to reach handling strength before the next dip. The required time depends on layer thickness, sand grade, and room conditions. Ganoksin forum practitioners report a working schedule for a five-layer shell.
Layer Sand grade Drying time Notes First layer medium molochite sand (60’s grade) about 1 hour in warm, dry conditions; using a cold fan helps speed drying Second layer medium molochite sand (60’s grade) about 40 minutes catches detail on the wax; could be omitted if the first layer was already perfect Subsequent coarse layers (two or three more) coarse molochite sand (16/30’s grade) about 30 minutes each used to build up the thickness of the shell Ganoksin reports that five layers at about 4 mm total thickness prove amply strong even for 15 kg sculptures. A minimum of one fine layer and two coarse layers serves jewelry work when the operator has a practiced, delicate touch. The chart below shows the same schedule in visual form.
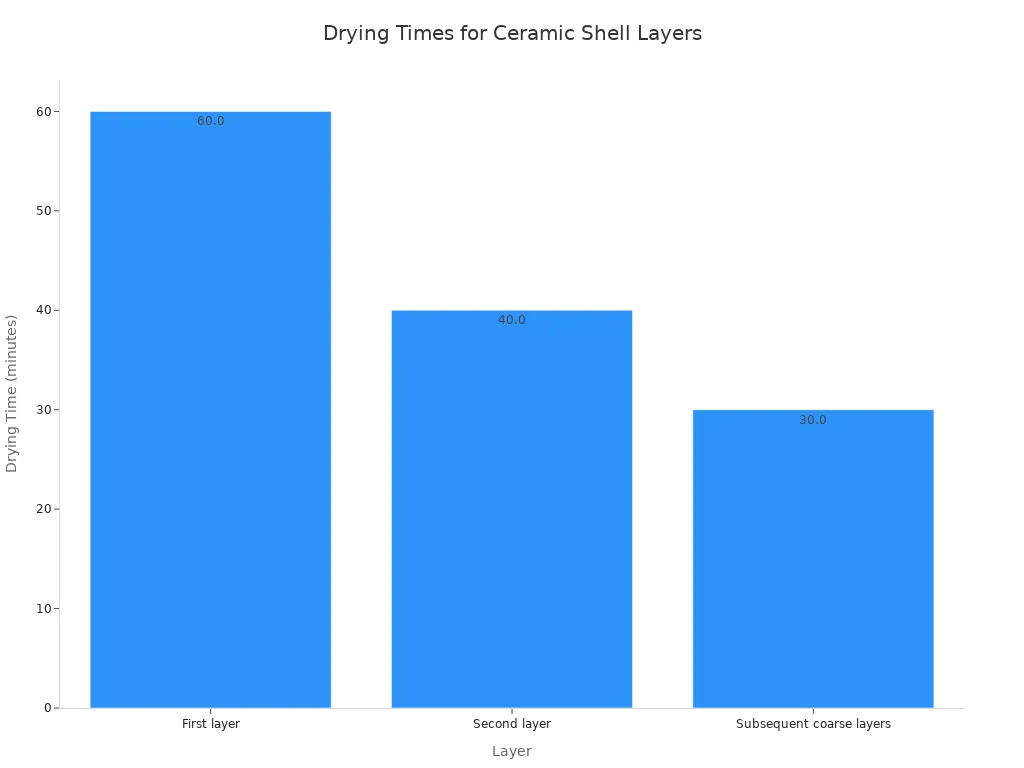
Image Source: https://www.xuxiangtaimetal.com The pattern in the data deserves attention. The first layer takes the longest because it sits directly on the wax and carries the surface finish. Later layers dry faster because the porous stucco beneath them wicks water away. This schedule assumes warm, dry conditions and forced air. A cold, humid shop stretches every interval. Engineers should set drying time by measured weight loss or residual moisture, not by the clock alone. A fixed schedule works only inside a fixed room condition.
Layer count and drying time trade against each other. More thin layers dry faster per layer and build less stress per pass. Fewer thick layers save handling time and raise the crack risk. The right balance depends on part geometry, alloy, and the firing profile that follows.
Detecting Incomplete Drying
An under-dried shell looks acceptable and fails later. The trapped water flashes to steam during dewaxing or firing, and the pressure splits the shell or blows ceramic into the cavity. Detection must happen before the shell leaves the drying room.
Weight loss gives the simplest signal. Operators weigh a control shell after each layer and compare the reading against a baseline for that layer. A shell that stops losing weight has reached equilibrium with the room. A shell that keeps losing weight is still drying. Residual moisture meters give a direct reading on thicker sections and on the sprue cup.
Visual and tactile checks catch gross errors. A properly dried layer feels chalky and does not smear under a gloved finger. A damp layer feels cool and shows a darker tone in recessed areas. Inspectors should check the deepest cavities and the underside of the tree, where airflow is weakest. These zones dry last and fail first.
The firing curve offers a final safety net. A slow preheat ramp lets residual moisture escape before the shell reaches sintering temperature. Patsnap notes that gradual preheating phases prepare the shell for the main firing cycle. A fast ramp removes that margin. Engineers who skip the moisture check should at least hold the preheat stage long enough to drive off the remaining water.
Step 5: Dewaxing
Dewaxing removes the pattern and leaves a hollow cavity that mirrors the final part. Gravity Cast India describes the step plainly: “The wax inside the newly built shell is now removed so the ceramic covered shell outer wax tree will be with hollow mirror cavity of the cast parts. Dewaxing is done using a steam-dewaxing autoclave or flash fire furnace.”
Autoclave versus Flash Fire Dewaxing
The two methods differ in speed, wax recovery, and shell stress. Patsnap reports that flash dewaxing heats the shell to roughly 150–200°C and ejects wax in 15–30 minutes. Steam autoclaves need 2–4 hours.
Attribute Flash Dewaxing Steam Dewaxing (Autoclave) Wax recovery rate 95–98% 85–90% Cycles per shift 8–12 2–3 Cycle time 15–30 minutes 2–4 hours Defect rate 30–50% lower Baseline Equipment cost Higher Lower Flash dewaxing suits high-volume lines that need fast turnaround. Autoclaves fit small-scale operations where longer cycles are acceptable.
Preventing Shell Cracking
Most wax expansion occurs between 120°C and 180°C. Patsnap recommends slow heating rates of 10–15°C per hour through this range to prevent pressure buildup. Vastpe reports that steam entering in under 7 seconds melts the outer wax boundary first and holds shell rejection below 0.5%. Controlled depressurization at 15–30 psi per minute further reduces cracking risk.
Wax Removal Verification
Operators inspect each shell after dewaxing for residual wax, cracks, and cavity damage. A clean cavity with sharp internal detail confirms complete removal. Any shell showing trapped wax or surface cracks goes to scrap before firing.
Step 6: Firing the Shell
Firing turns the dried shell into a rigid ceramic mold. Heat burns out residual organics and sinters the refractory particles into a bonded structure. The cycle design decides final strength, thermal stability, and crack resistance.
Sintering Temperature and Cycle Design
The firing cycle runs in two stages. Zhycasting.com reports that organic decomposition occurs between 200–800 °C. Operators hold the shell in this range so organic matter escapes slowly. The heating rate between 200–600 °C should stay at 2–5 °C/min. A faster rate releases gas too quickly and cracks the shell. Final sintering follows at 1300–1500 °C.
Stage Purpose Temperature Notes Organic decomposition Remove organic species 200–800 °C Hold at 2–5 °C/min in the 200–600 °C window Final sintering Develop ceramic bonding 1300–1500 °C Uniform temperature distribution and controlled heating rates Strength Development and Thermal Stability
Sintering is a solid-state diffusion process. Kindle-tech.com explains that atoms diffuse across particle boundaries, close pores, and weld grains into a dense polycrystalline structure. Densification raises mechanical strength and hardness. A well-sintered shell has minimal internal voids, so cracks cannot initiate or propagate easily. Strong atomic bonds also give the shell excellent thermal stability for high-temperature alloys.
Cooling and Handling After Firing
Cool-down needs control as much as heat-up. A fast drop in temperature creates thermal gradients across the shell wall. Operators should let the shell cool inside the kiln or in a covered zone. Handling follows only after the shell reaches a safe temperature. Gloves and padded supports protect the hot ceramic from mechanical shock.
Why Ceramic Shells Support Reliable Castings
Dimensional Accuracy and Surface Finish
Ceramic shells capture fine detail from the wax pattern and hold that geometry through pouring. Aerometals reports that investment casting delivers surface finishes of approximately 125 RMS and typical linear tolerances of ±0.005 to ±0.010 per inch, depending on alloy and geometry. The prime coat does most of this work. Sefu notes that zircon and fused silica in the first two layers create a smooth, dimensionally accurate surface replica, while backup coats of molochite and mullite build strength and permeability. Zircon brings low thermal expansion, a key advantage for precision work. Texmo Blank adds that ceramic molds resist distortion and capture intricate designs without extensive post-processing.
Thermal Resistance for High-Temperature Alloys
A ceramic shell must survive thermal shock during pouring and resist reaction with the molten alloy. Zhycasting reports that zircon face coats show a coefficient of thermal expansion of 4.5–5.5 × 10⁻⁶/°C and flexural strength of 30–50 MPa. Fused alumina offers higher strength at 50–80 MPa but a higher expansion of 7.0–8.5 × 10⁻⁶/°C. Superalloys expand at roughly 12–14 × 10⁻⁶/°C, so graded shell structures and compliance layers absorb the mismatch. Low-expansion refractories keep thermal stress inside the shell’s tolerance.
Process Consistency Across Production Runs
Repeatability separates a reliable foundry from a lucky one. Slurry viscosity, stucco gradation, drying room setpoints, and firing profiles must hold inside defined bands on every run. Each layer adds a controlled increment of thickness and strength. Engineers who log these variables and compare them run to run catch drift before it reaches the pour. Consistent shells produce consistent castings, and consistent castings keep tolerances and surface finish inside the values the process promises.
Common Challenges and How to Mitigate Them
Shell-making defects follow predictable patterns. Engineers who recognize the pattern can correct the cause instead of chasing the symptom.
Shell Cracks and Their Causes
Cracks usually trace back to stress the shell cannot absorb. Rapid drying hardens the outer skin before the interior loses its water, and the shrinkage gradient opens a fissure. Thermal shock during pouring produces the same result when a turbulent metal stream erodes the gating system. Sefu recommends a controlled, diffused pour through a ceramic pouring cup to calm the metal stream and protect shell integrity. Slow heating through the 120–180°C wax expansion range also limits internal pressure during dewaxing.
Inclusions and Surface Defects
Foreign material enters the cavity through several paths. Barron Industries reports that slag and sand inclusions are the two most common types, and the company counters them with automated temperature and humidity control, daily slurry testing, deoxidizing practice before tapping, and ceramic filters sized to trap fine particles. Rough or decarburized surfaces respond to preheated shells and a reducing atmosphere after pouring. The table below summarizes the main defects and their countermeasures.
Defect Source/Cause Prevention Inclusions (ceramic or slag) Shell fragments or melting dross trapped in the casting Final filtration barrier with an inert zirconia ceramic foam filter in a ceramic pouring cup Wax residue (ash) inclusions Incomplete burnout leaving carbonaceous residue Complete dewaxing and burnout; high-purity crucible and final filtration Surface roughness (fins or veins) Shell cracks filled by metal after thermal shock Minimize thermal and mechanical shock; diffused flow from a ceramic pouring cup Mold crack or metal penetration Thermal shock and turbulent metal stream Calm the metal stream to reduce erosive first impact Secondary oxide scum Turbulent pouring re-oxidizes the stream Laminar, protected flow from cup through filter Dimensional Drift and Layer Control
Dimensional drift accumulates quietly across layers. Slurry viscosity outside its window changes pickup per dip, and shell thickness wanders from the target band. Uneven stucco gradation compounds the error. Daily viscosity and specific gravity checks, fixed drain times, and thickness measurement after each layer hold the shell inside tolerance. Logging these values run to run exposes drift before it reaches the pour.
Reliability in investment casting builds layer by layer, from wax pattern preparation through firing. Slurry control, drying discipline, and firing accuracy are core requirements, not optional refinements. Engineers who write a professional B2B technical article about ceramic shell making in investment casting. Target audience: American mechanical engineers should treat every step as a quality checkpoint with defined acceptance criteria.
FAQ
How many ceramic shell layers does a typical investment casting need?
Most stainless steel castings use five to seven layers. Small parts need fewer. Large or heavy parts need more backup coats for strength.
Why do ceramic shells crack during dewaxing?
Wax expands rapidly between 120°C and 180°C. A slow heating rate of 10–15°C per hour lets the shell relieve internal pressure and avoid cracks.
How does a foundry verify shell quality before pouring?
Operators check shell thickness, surface condition, and cavity cleanliness after firing. Cracks, residual wax, or thin spots send the shell to scrap.
See Also
How To Avoid Selecting The Wrong Aluminum Casting Process Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.