- This topic is empty.
-
AuthorPosts
-
2026-11-10 at 5:01 pm #12987
Understanding Two Distinct Tensile Metrics
Cosmetic packaging buyers reviewing a tensile test report often see two figures listed close together — strain at yield and elongation at break — and assume they describe the same property. They do not. Each metric captures a different stage of a plastic specimen’s response to pulling force, and conflating them can lead to incorrect assumptions about how a compact hinge, a lipstick tube wall, or a lip gloss tube thread will actually behave in the field.
Strain at yield marks the point on the stress-strain curve where the material transitions from elastic (fully recoverable) deformation to plastic (permanent) deformation. Before this point, if the load is removed, the specimen returns to its original shape. After this point, the material has begun to permanently stretch or deform, even though it has not yet failed. For rigid packaging plastics such as PMMA or AS, strain at yield is typically a small percentage, reflecting their relatively stiff, less forgiving nature.
Elongation at break, by contrast, describes the total strain the material has accumulated at the moment it physically fractures or separates. This number includes both the elastic deformation and all of the plastic deformation that occurred after yield, right up until failure. A material can have a low strain at yield but a comparatively higher elongation at break if it exhibits ductile behavior — stretching considerably before it finally snaps.
Why the Distinction Matters for Packaging Components
The gap between these two values tells an engineer whether a material behaves in a brittle or ductile manner once it is pushed past its elastic limit. A narrow gap between strain at yield and elongation at break signals a brittle material: once yield is reached, failure follows quickly, with little warning deformation. A wide gap signals a ductile material that visibly deforms before it ultimately breaks.
This distinction is directly relevant to compact powder case hinges, where living-hinge designs rely on a material’s ability to flex repeatedly without reaching its elongation-at-break limit, while pin-hinge designs place different stress patterns on the housing material. Material science work that evaluates living hinge vs pin hinge performance depends on understanding where a candidate resin sits on this spectrum — a resin with adequate elongation at break but a very fast transition past yield may still be unsuitable for a living hinge that must flex thousands of times without cracking.
Similarly, for clear compact lids, the choice between AS and PMMA is informed partly by these two metrics. PMMA generally offers higher optical clarity and stiffness but tends toward lower elongation at break, making it more prone to brittle fracture under impact. AS resins can offer a different balance of clarity and toughness. Reviewing both strain at yield and elongation at break on a supplier’s tensile report — rather than clarity or gloss alone — gives a more complete picture of how a lid will hold up during shipping, drop impacts, or repeated opening and closing.
Standard Test Conditions Behind the Numbers
Tensile data for packaging plastics is typically generated using standardized methods such as ASTM D638 or the ISO 527 series, which specify dogbone-shaped specimens, defined gauge lengths, and controlled crosshead speeds during testing. Because polymer behavior is sensitive to testing speed and environment, a credible report should state:
- Specimen type and dimensions, since thinner-walled packaging components may be tested with reduced-size specimens that do not always correlate directly to bulk material data.
- Crosshead speed, as faster pulling rates tend to reduce apparent elongation at break and can raise apparent yield stress, meaning two reports run at different speeds are not directly comparable.
- Conditioning temperature and humidity, since many plastics used in cosmetic packaging — including PCR/PET, PETG, PMMA, and AS — absorb moisture or shift in stiffness with temperature, which affects both yield behavior and ultimate elongation.
- Reference standard, since ASTM and ISO methods calculate strain measurement slightly differently and are not interchangeable without noting the method used.
Without this context, a single percentage figure for elongation at break is difficult to interpret responsibly. A buyer comparing two resin options should confirm that both reports were generated under matching conditions before drawing conclusions about relative toughness.
Reading the Limits, Not Just the Numbers
"Limits" on a tensile report generally refer to the specification thresholds a brand or converter sets for a given component — for example, a minimum acceptable elongation at break for a hinge component intended to flex repeatedly, or a maximum permissible strain at yield for a rigid wall section that must not visibly deform under normal handling. These thresholds are application-specific and are typically defined jointly between the packaging engineer and the material supplier based on the component’s function, rather than being universal constants across all cosmetic packaging. A threshold suitable for a rigid outer shell is not automatically appropriate for a flexible hinge or a threaded closure subject to repeated twisting, such as those prone to leakage from wiper interference and heat expansion in lip gloss tube threads.
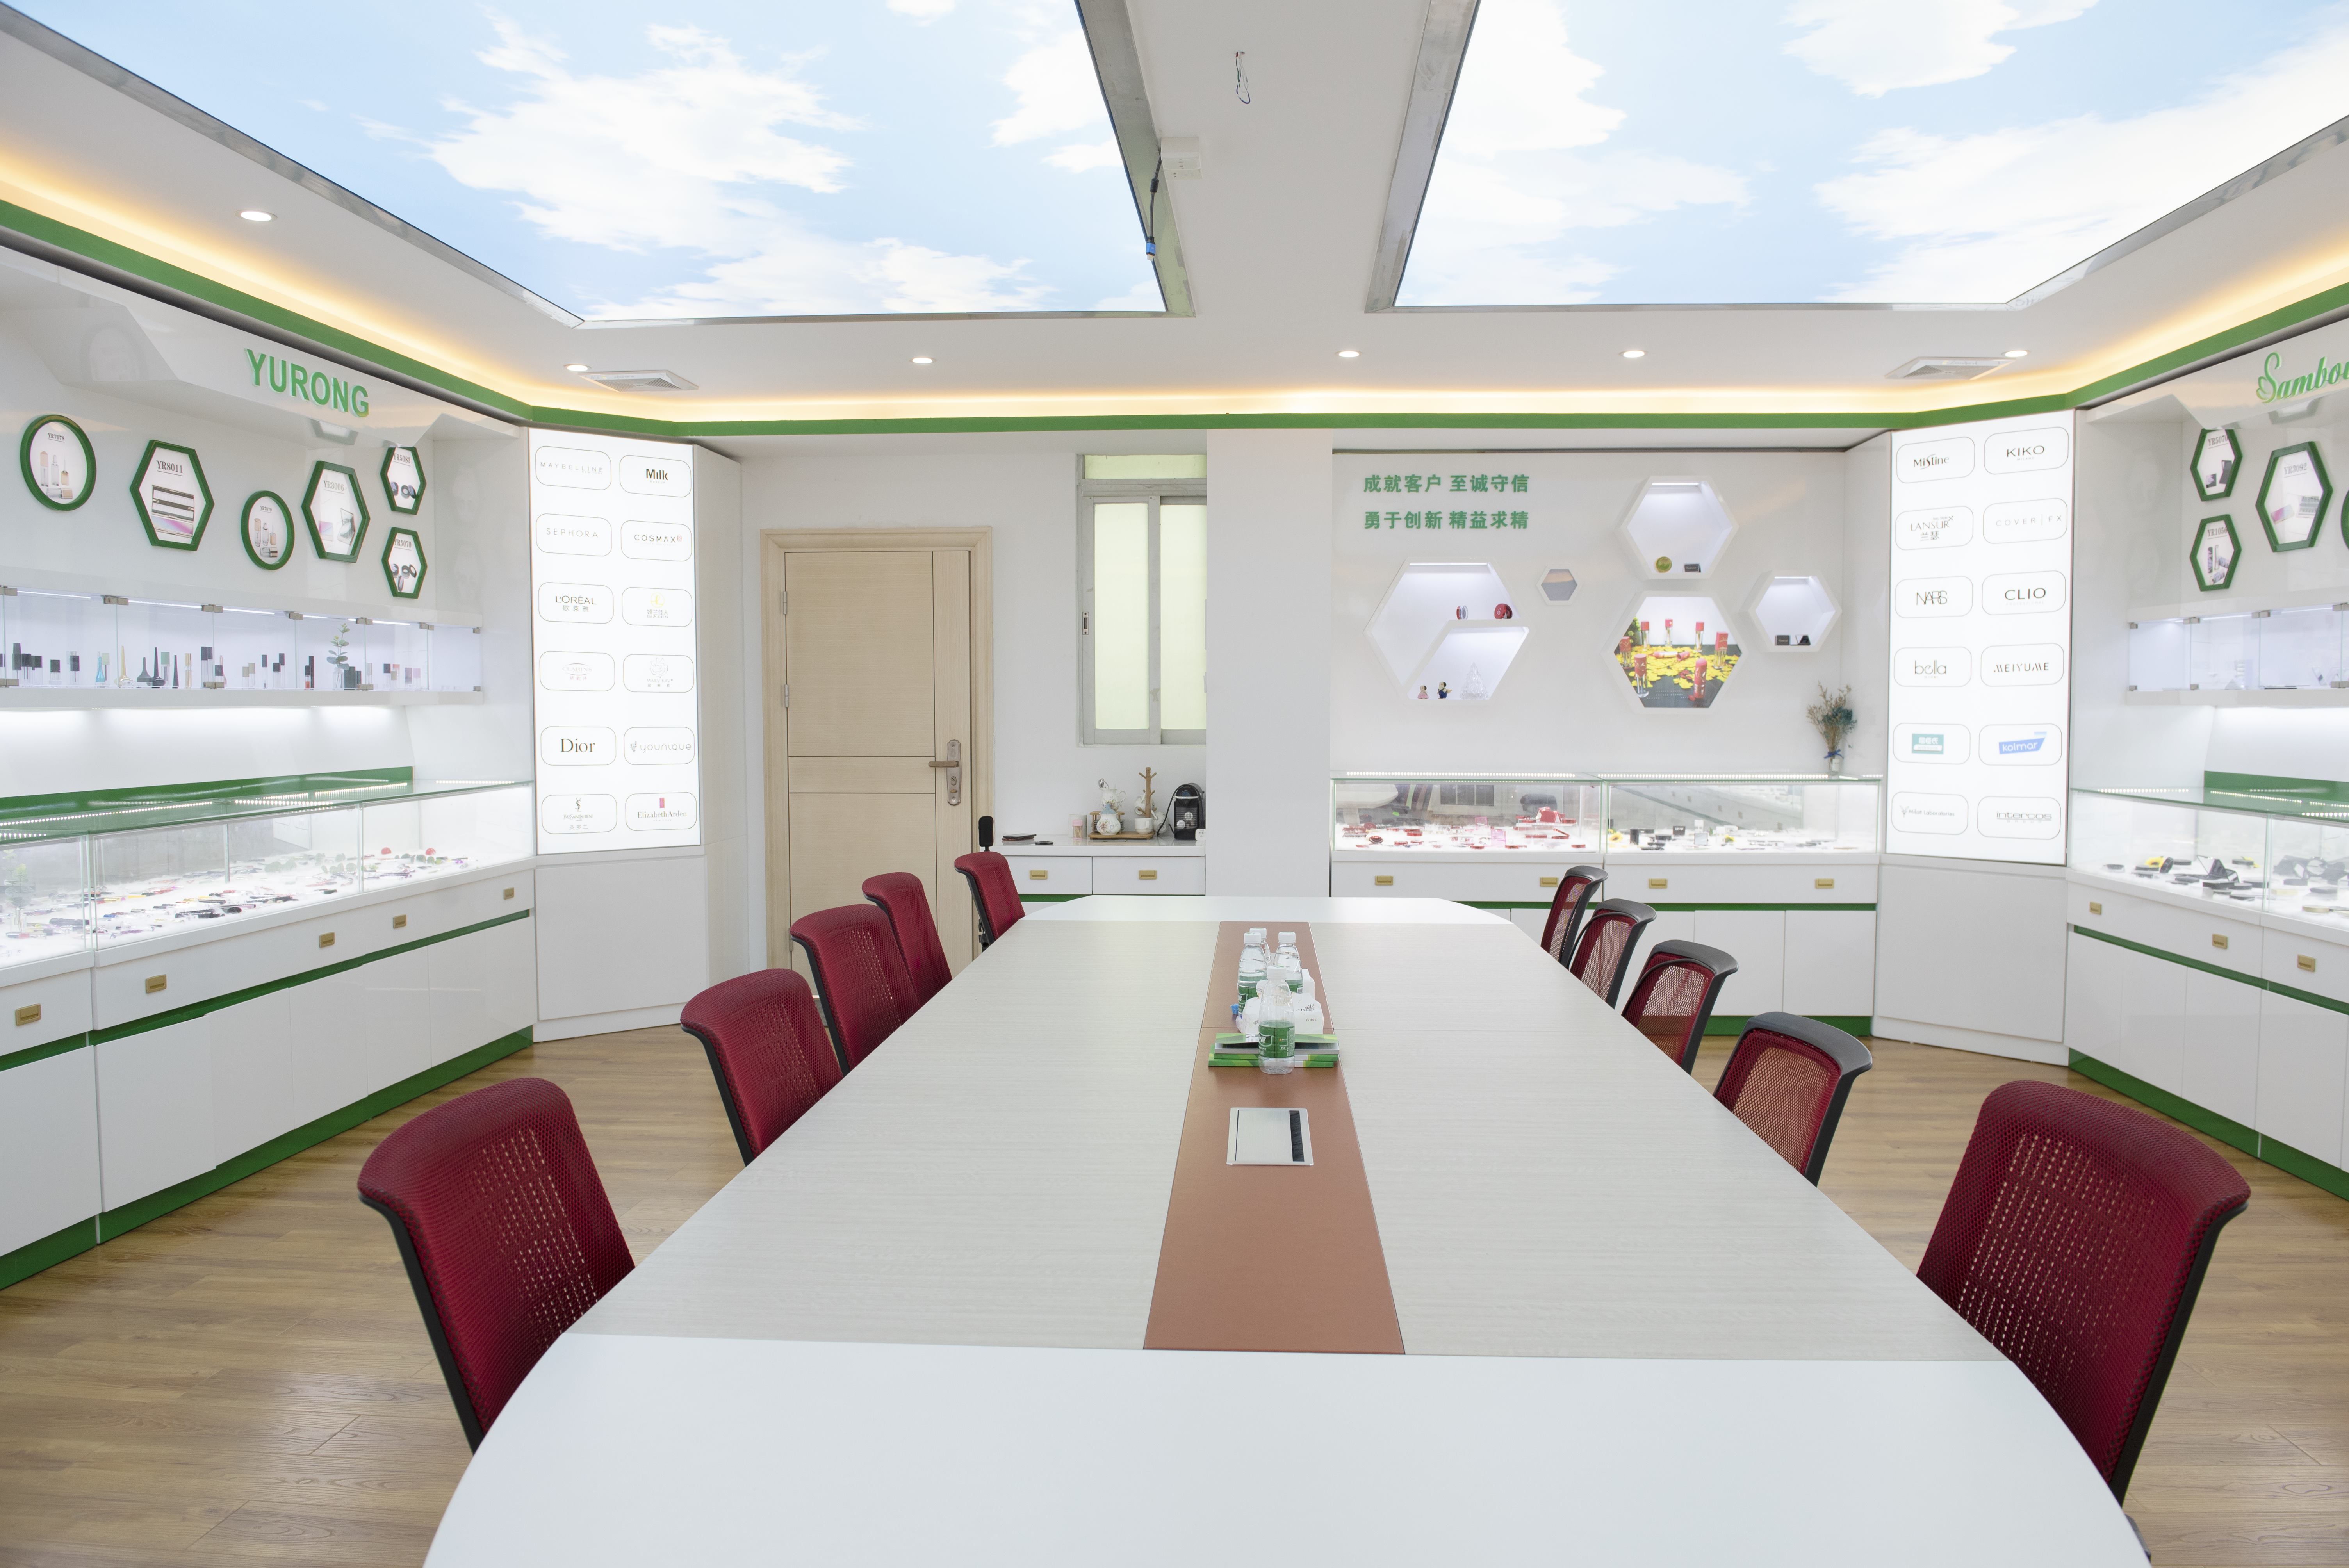
Context, Not Substitution: The Showroom Photo
A showroom photo of finished compact cases, lipstick tubes, or metal packaging communicates surface finish, color, and overall aesthetic presentation — useful context for evaluating decoration quality such as vacuum metallization, electroplating, or silk screen printing. It does not, however, provide any information about mechanical performance. Two components can look identical on a showroom shelf while using different base resins with very different strain-at-yield and elongation-at-break profiles. Aesthetic inspection and tensile reporting answer different questions, and one should not be substituted for the other when qualifying a packaging component for production.
Practical Takeaway for Packaging Buyers
When reviewing a tensile report for cosmetic packaging plastics, procurement and quality teams benefit from asking for both strain at yield and elongation at break side by side, along with the test standard, specimen details, and conditioning parameters used to generate them. This is particularly relevant for manufacturers working across multiple polymer options — including PCR/PET, PETG, PMMA, AS, aluminum, and zinc alloy — where material selection directly affects hinge durability, lid impact resistance, and thread integrity. Companies such as Dongguan Sambound New Material Technology Co., Ltd., which engage in structural integrity engineering for leakage prevention and hinge durability as part of material selection between AS and PMMA, illustrate how these two tensile metrics feed directly into real packaging decisions rather than remaining abstract laboratory figures. Understanding the difference, and insisting on complete test documentation rather than appearance alone, helps packaging teams avoid field failures that a showroom photo alone could never reveal.
sambound.com
SamBound New Material Technology Company Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.